
What Is the Pantone Matching System?
The Pantone Matching System, usually shortened to PMS, is a standardized color reproduction system for spot inks. Each color carries a unique number and a documented formula specifying the proportions of base pigments used to mix it. A designer specifies the number; any printer holding the matching Formula Guide can mix the same ink.
Lawrence Herbert joined Pantone in 1956 as a part-time color matcher, acquired the company’s technology assets in 1962, and introduced the first Pantone Matching System fan book in 1963, built from a small set of base inks and each color carrying a published mixing formula (Pantone). The problem it solved was mundane and expensive: before it, matching a color across suppliers or across a year meant sending a physical sample and hoping. The current Formula Guide, the coated and uncoated reference used across print and packaging, carries roughly 2,390 spot colors (Pantone Formula Guide).
Worth being precise about what that achievement was. Pantone standardized the specification. It did not standardize the result, and it never claimed to. Arkay has been holding brand color on paperboard since 1922, and the distance between those two things is most of what a color-critical program is actually buying. A number tells a printer which ink to mix. It says nothing about the board that ink lands on, the pressure it is transferred under, or the light somebody judges it in. Every difficulty in the rest of this article follows from that distinction.
The Pantone Palettes, and Which Ones Apply to Packaging
Pantone does not publish one library. It publishes several, built for different materials, and only some of them are relevant to a folding carton.
The coated and uncoated print libraries are the pair that matter. They carry the same spot ink formulas but show them printed on two different surfaces, which is why a number appears with a C or a U suffix. Coated stock holds ink largely on the surface and reads brighter and more saturated. Uncoated absorbs it into the fiber and reads softer. Pantone’s own explanation is worth quoting, because it settles a common argument: on coated paper ink “sits atop the coating allowing for minimal ink absorption,” on uncoated there is “no surface coating permitting maximum ink absorption,” and “the majority of the difference is attributed directly to the reaction of the ink to the paper” (Pantone).
Two consequences follow. The same number in C and U form is not the same visual color, and a specification should always name the suffix matching the board actually being printed.
There are also process versions of the libraries, which show the CMYK build that approximates a spot color rather than the spot ink itself. Those are useful for knowing what a color will look like if it is not run as a spot, and they are not a substitute for the spot formula.
Beyond print, Pantone maintains textile and plastics libraries with their own suffixes. They serve fashion, interiors, and molded components. They are not packaging references, and specifying one on a carton is a common and avoidable error.
Why Brands Specify Pantone Colors
Three reasons, in roughly the order procurement cares about them.
Precision. A spot ink is mixed to a formula rather than reconstructed from four screens, so it lands closer to the target and stays there across a run.
Reach. A significant share of the Pantone library sits outside what four process inks can mix, particularly saturated blues, oranges, violets, and anything fluorescent. For those colors, spot is not a preference, it is the only route.
A shared reference. The number means the same thing to a designer, a brand manager, and a printer who have never spoken. That is the part the system actually solved, and it is why it survived sixty years of everything else in printing changing.
Why the Same PMS Number Prints Differently
A designer signs off a chip. The carton arrives. The color is close but not the same, and nobody can explain why. There are six mechanisms, and they stack.
1. Substrate Absorption
Coated board keeps ink largely on the surface, producing a brighter, more saturated result. Uncoated absorbs it into the fiber, producing something softer and duller. This is not a defect in either direction. It is why Pantone issues two chips for one formula.
2. Board White Point
Every printed color is the ink film plus whatever the sheet contributes underneath it and through the gaps between halftone dots. Paper brightness is among the substrate attributes with the most direct effect on printed color, and the relationship is not linear: color rendering improves with whiteness only up to a point, after which further brightness stops helping (BioResources).
The practical consequence is that a shift in the board shifts every color printed on it. Light tints, pastels, and large flat fields feel it most, because those are the areas where the substrate contributes the largest share of what the eye receives.
3. Ink Film Thickness
Solid ink density is a proxy for how much ink is actually on the sheet, and it moves two things at once. Raising density raises saturation, and it also raises dot gain. The two are coupled, which means a press operator correcting one perceived problem can worsen another, and why density is held to a target rather than adjusted by eye.
4. Dot Gain
Halftone dots enlarge between plate and board. How much depends on ink film thickness, dampening, screening choice, dot shape, and the absorbency of the substrate. On any color built from screens rather than a solid, dot gain moves the result.
5. Metamerism and Light
Two colors can match under one light source and visibly disagree under another. This is not perception failing; it is spectral reality, and it is the reason standardized viewing conditions exist as a formal standard. ISO 3664:2009 specifies a D50 illuminant at 5000K, requiring a color rendering index above 90 and holding metamerism indices to strict limits (ISO 3664:2009).
Practically: a client rejecting color under their office fluorescents, or a photographer approving it under a studio strobe, are both making a judgment the standard was written to prevent. The light is part of the measurement.
6. Gamut and Coating
Some Pantone colors cannot be reached with four process inks at all. Their pigment bases, particularly saturated blues, oranges, violets, and anything fluorescent, sit outside what cyan, magenta, yellow, and black can mix. Specifying such a color as a process build produces a visible miss before the press even starts.
And the last layer changes the answer again. An overprint varnish or aqueous coating alters gloss, and gloss alters perceived saturation and depth. A color measured bare and the same color measured under coating are not the same reading.
The one-sentence version: the chip is one ink, on one substrate, under one light. Production changes all three, each shift is small, and they compound.
Pantone Versus CMYK on a Folding Carton
Three routes to a color on a folding carton, and the choice belongs in prepress rather than in the design file.
Spot means a pre-mixed ink on its own press station. It is the right answer for brand-critical color: a logo, a signature panel, anything a customer would recognize as wrong. It reaches colors process cannot, and it removes the four-plate registration and overprint math from the equation entirely.
Process builds color from screens of cyan, magenta, yellow, and black. It is the right answer for photographic imagery and gradients, where a spot ink cannot do the work anyway.
The cost lever is stations. Each additional spot color is another plate, another wash-up, another element of make-ready, and on a multi-version job those repeat. That is the real trade-off a procurement lead is weighing, and it is why the spot-versus-process decision should be deliberate rather than inherited from whatever the design file happened to contain.
For high-volume lines running many SKUs, a fixed expanded ink set changes the arithmetic again by reaching a wide gamut without a plate per shade. We cover that route and its trade-offs separately in our guide to extended gamut printing.
How Color Accuracy Is Measured
This is where the conversation gets useful, because it replaces opinion with numbers.
Densitometers versus spectrophotometers. A densitometer reads reflected light through colored filters. It is fast and has been the on-press instrument for decades, and it answers a narrow question: how much ink is down. A spectrophotometer captures the full visible spectrum and computes Lab values, which are a numeric description of a color that means the same thing on any instrument and in any plant. That difference is what makes color communication possible across substrates, suppliers, and continents, because a Lab value travels while a density reading does not.
Delta E and tolerance. Delta E expresses the distance between a measured color and its target as a single number. The current formula is ΔE2000, which supersedes the older ΔE76 because it corresponds more closely to how human vision actually weights differences (Printing United Alliance). The working convention is well established: below 1.0 is imperceptible, below 2 is very good, 2 to 3 is generally acceptable, and above 3 becomes visibly noticeable and usually triggers a correction (ASAS Label).
It is worth being precise about where these numbers come from, because they are routinely misattributed. ISO 12647-2:2013 governs process control for offset lithography, and its tolerances apply to the process primaries, to tone value increase, and to gray balance. It does not set spot-color tolerances. Tolerance on a brand color is agreed between brand and printer, and brand-critical programs commonly work to a Delta E of 2 or tighter by agreement. On the proofing side, ISO 12647-7:2016 does set a figure: a Delta E of 2.5 for measured spot colors (proofing.de).
What matters more than the specific figure is that somebody names one, in writing, before the run. A tolerance agreed in advance turns color approval into a measurement two parties can both take. Without one, approval is a conversation about whether something looks right, which nobody wins.
Draw-downs on the actual substrate. A draw-down applies the mixed ink to the real production board, and it exists because it is the only way to see what an ink genuinely looks like on a given surface (PrintWiki). Approving a color against a generic proofing stock, and then printing on 18pt board with a coating over it, is approving a different thing from what will ship.
Closed-loop control during the run. Where a plant runs it, inline spectrophotometers read a color bar on the moving sheet and feed corrections back to the ink keys continuously rather than sampling after the fact (Techkon). The difference is between discovering drift and preventing it, and it is a fair thing to ask a supplier about directly.
Retained masters for repeat runs. A physical approved sample, kept and measured against on every reorder, stops slow accumulation. Without one, each run is measured against the run before it, and a series of individually acceptable steps can walk a long way from where it started.
What G7 Certification Covers
G7 is frequently described as though it promised color matching. It does not, and the distinction is worth getting right because overstating it is how trust gets lost.
G7 is a calibration methodology. It defines a shared neutral appearance through the Neutral Print Density Curve, referenced to the media white point, along with gray balance targets, and it prescribes how to calibrate any printing or proofing system toward that appearance (Idealliance). It explicitly does not specify ink colors. It controls the starting point.
The stack is easier to follow as three layers. G7 is the methodology for getting a press to a known, measured state. GRACoL and FOGRA are the reference conditions, the datasets defining what the target output should be. ISO 12647-2 is the international standard the whole arrangement answers to.
Why a brand should care is specific: a G7-certified press begins each job from a documented baseline rather than an assumed one. That is the precondition for repeatable color, not a substitute for measuring it. G7 Master Facility qualification is also a plant credential, verified through submitted measurement data and independent evaluation, which is a different thing from selling the software that helps printers hit the curves.
How Brands Govern Color Across Suppliers
Sophisticated brands have largely stopped treating a physical chip as the single source of truth, for a straightforward reason: even with identical substrate, ink, and process specified, different converters in different locations do not produce the same color from a physical guide alone.
The practices that hold up:
- Measure the approved target and distribute the data. Spectrally measure the physical standard once and issue the full spectral data to every supplier, rather than posting chips and hoping (X-Rite).
- Specify numerically, not descriptively. Communication with converters should name target Lab values instead of subjective direction. “Warmer red” cannot be verified; a Lab value can (X-Rite).
- Set tolerances per substrate. One Delta E window across cartons, labels, and shippers ignores that the substrates behave differently. Name a tolerance for each (Datacolor).
- Define ICC profiles for process imagery so photographic elements are handled deliberately rather than converted at output.
There is a structural observation buried in that first point. Every supplier added to a program adds a set of variables: a different press, a different board source, a different measurement habit. Reducing the number of places a color is produced is not a quality claim, it is arithmetic.
How Arkay Holds Brand Color Through a Run
Arkay has been printing paperboard since 1922, now in its fourth generation of family ownership.
Four things are worth stating plainly, because they are the ones that are documented.
G7 color management certification. In Arkay’s own terms, it means every press job is profiled against a neutral gray balance before a production run begins. The plate calibration curves applied upstream in packaging prepress are matched to the press that will receive them. As set out earlier, G7 controls the starting point. It is not a claim about any individual Pantone number, and it is verified by a third party rather than self-declared.
One substrate family. Printing runs offset on solid bleached sulfate board from 14 to 28pt, with 28pt as a hard ceiling. That narrowness is the point: board white point, absorbency, and dot gain behavior are known quantities rather than variables reintroduced with every job. The behavior of that substrate is covered in our guide to paperboard packaging.
One facility. All of it happens in a single 140,000 sq. ft. carbon-neutral plant in Roanoke, VA. Fewer places a color is produced means fewer variables to manage.
Paint on Press. Where a color needs more than a flat ink can give, Paint on Press is Arkay’s proprietary process, developed under Chairman Emeritus Howard Kaneff, running up to 20 variations. It lets a brand push past a single specified shade without pushing past a controlled process, and it sees the most use in cosmetics and beauty programs where a signature color carries the brand.
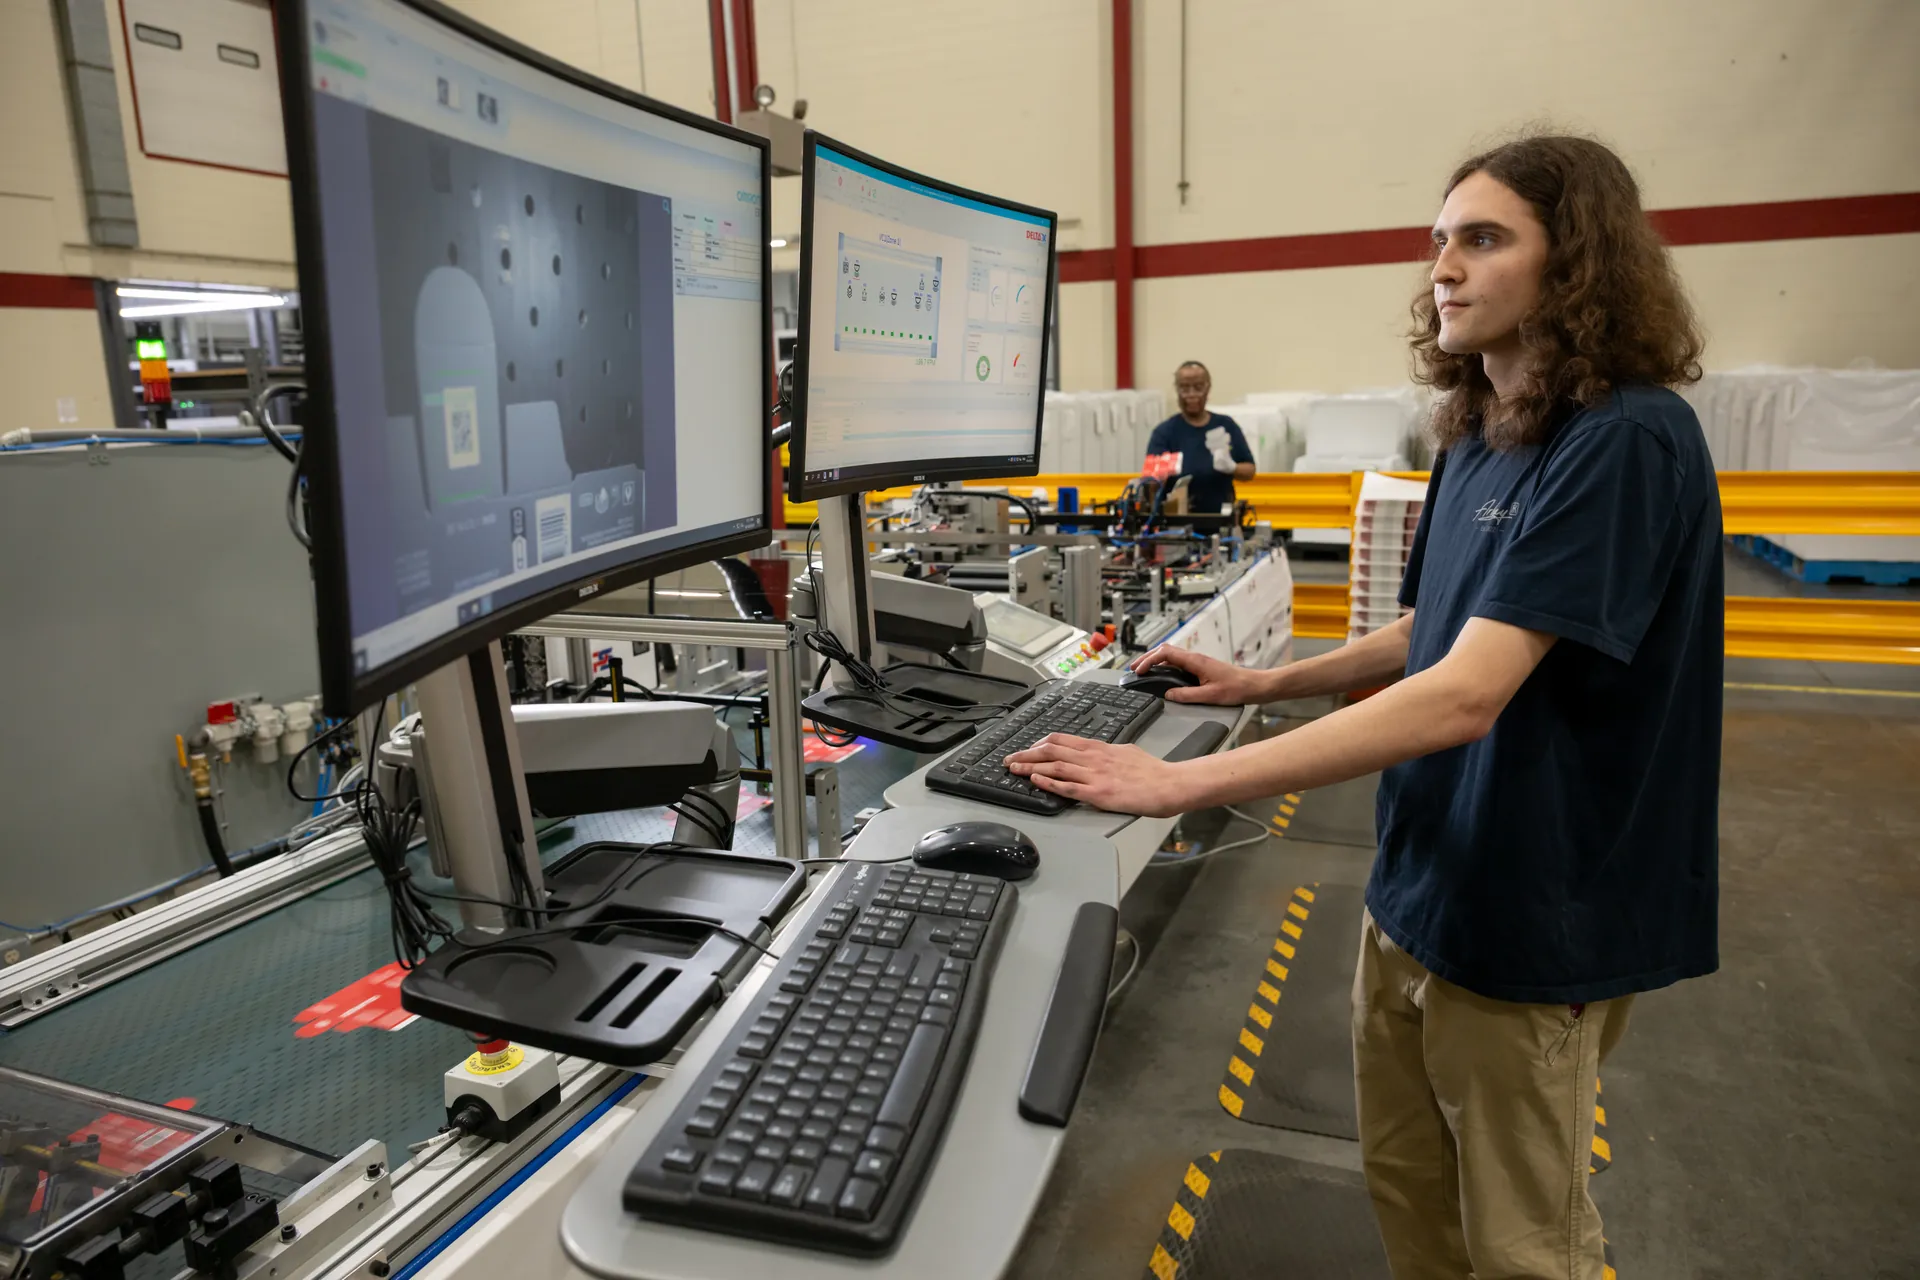
Closed-loop spectrophotometric color control on every press. Arkay runs four presses, and all four measure color instrumentally and correct against the reading rather than against an operator’s eye. The newest system, Inpress Control, runs on one of them and measures the color bar on the sheet while the press is running, feeding corrections back to the ink keys continuously. The other three run Image Control, which scans the printed sheet spectrophotometrically and feeds the correction back to the press. The distinction is worth understanding rather than glossing: one prevents drift as it happens, three catch it against a measured standard rather than a remembered one. Both are measurement, and neither is judgment.
That covers the instrument side. On the remaining controls described earlier in this article, an agreed working Delta E tolerance, standardized D50 viewing, draw-downs on the production substrate, and retained masters for repeat runs, the right thing to do is still ask, of Arkay as of anyone. Those are the controls the industry works with, and a supplier should be able to tell you which of them sit in its process. Our guide to packaging quality assurance covers how in-process checks are structured.
Arkay’s team works alongside brand teams, designers, and packaging engineers to set a target the board can actually hold, which is a more useful conversation than agreeing to a number and discovering the substrate later.
Bring Us Your Brand Color
Bring the number, and bring the board it has to print on. Those two things together are a specification. On their own, either one is a hope.
If the color already exists and keeps drifting between suppliers, the fastest way in is a measured target on the actual sheet rather than another round of comparing chips under whatever light is in the room.
Reach out to Arkay’s team to talk through color specification, or ask us directly which measurement controls we run on your job.
Frequently Asked Questions
Which packaging manufacturers can hold Pantone color accuracy across runs?
This one is general guidance for evaluating any supplier, rather than a description of one. Look for three things rather than a promise. First, G7 color management certification, which means the press is calibrated to a documented gray-balance baseline before any brand color is loaded. Second, measurement rather than judgment: spectrophotometric readings against an agreed Delta E tolerance, with standardized D50 viewing conditions and draw-downs on the actual production substrate. Third, structural simplicity: fewer places a color is produced means fewer variables to manage. Anyone offering a guarantee instead of a measurement method is describing a commercial position, not a process.
How do you match a color to Pantone?
Compare against a physical Pantone Formula Guide under standardized D50 lighting, never against a screen and never under ordinary office light. Screens emit light while packaging reflects it, so a monitor match is not evidence of a print match. For production, the printer then draws down the mixed ink on the actual job substrate and measures it, because the same formula reads differently on different board.
Who should own the brand color standard, the brand or the printer?
The brand should own it, and should hold it as measured data rather than as a physical chip in a drawer. A printer can hold a retained sample and match to it faithfully, but if the brand has no independent standard, then the standard is whatever the last run happened to produce, and drift becomes invisible. The stronger arrangement is a brand-held Lab specification with an agreed tolerance, against which every supplier and every run is measured.
Is there a free Pantone color chart?
Free online charts exist, and Pantone publishes its own Color Finder, both showing approximate HEX, RGB, and CMYK equivalents. They are screen simulations rather than calibrated physical standards, which makes them useful for orientation and unreliable for approval. Any production decision should reference a physical Formula Guide viewed under standardized lighting.
How often should a brand re-measure its master color?
Whenever the physical reference could have changed, and at least at the start of any significant new program. Printed and painted standards fade with light exposure and handling, so a chip or sample kept for years is not necessarily the color it was when it was approved. A brand working from measured spectral data avoids most of this, because the data does not fade, but the physical sample used to generate it should still be stored away from light and replaced rather than trusted indefinitely.
Can a Pantone color be matched exactly?
Not exactly, in the strict sense, and it is more useful to think in terms of an agreed tolerance than a perfect match. Ink is mixed to a formula and laid on a specific substrate under specific press conditions, and each of those introduces a small amount of variation. What is achievable is a result close enough that the difference is imperceptible or commercially acceptable, measured rather than eyeballed. That is why a specification naming a target and a tolerance is more useful than one naming a Pantone number alone.